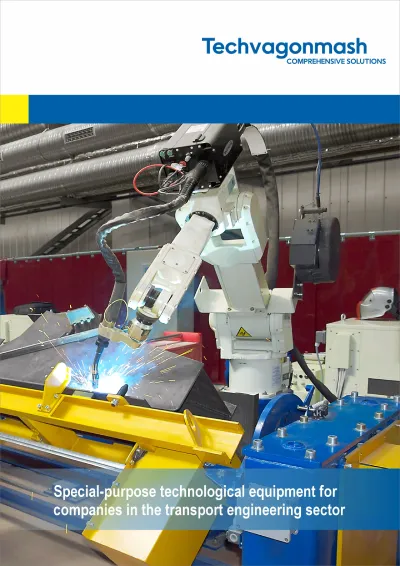
The stand is designed for automated submerged-arc welding of the longitudinal seam of a railway wagon center sill, combined with a pre-camber (pre-bend) operation that compensates for metal distortion caused by welding.
Design and Operating Principle
The complex consists of three units:
- Center sill welding stand with reverse camber capability — a rigid welded frame with pneumatic clamping, orientation, and vertical gripping mechanisms, a lever-type camber mechanism, and an adjustable retractable support.
- Transport system — a carriage with an electromechanical drive that moves the welding equipment along the stand at separate travel and welding speeds, regulated by a frequency converter.
- Control panel — a touchscreen panel for controlling the stand’s pneumatic equipment, plus a separate panel for controlling the Lincoln Electric welding package.
The center sill is loaded into the stand flanges-down, positioned longitudinally by a pusher and transversely by centralizers, then clamped vertically by pneumatic grippers before the pre-camber operation is performed. The welding head, mounted on the moving carriage, tracks the seam automatically using a light pointer; after welding, the camber and clamping cycle is reversed to release the part.
Advantages
- Real-time distortion compensation — the pre-camber is calculated for the specific sill geometry, removing the need for post-weld straightening.
- Precise geometry control — centralizers and side clamps hold the 350±1 mm dimension throughout the welding cycle.
- Flexible welding speed control — the frequency-controlled drive allows the mode to be matched to seam thickness and gap.
- Integrated Lincoln Electric welding package — power source, wire feed head, and flux recirculation system are supplied as part of the stand, with no separate integration required.
- Industrial-grade mechanism reliability — all core mechanisms are pneumatic, and the frame is a rigid welded construction.
Specifications:
| 1. | Welding stand: | |
| Center sill clamping mechanisms and orientation | Pneumatic | |
| Center sill deflection mechanism | Pneumatic | |
| Center sill vertical gripping mechanism | Pneumatic | |
| Support drive mechanism | Pneumatic | |
| Support type | Adjustable | |
| Support rotation angle, degrees | 90 | |
| 2. | Transport system: | |
| Platform motion drive | Electromechanical | |
| Drive capacity, kW | 1,1 | |
| Inoperative speed, m/min | 15 | |
| Welding speed, m/min | 0,4…0,7 | |
| Welding speed adjustment regulation | frequency | |
| Seam type | Butt-joint | |
| Welding method | SAW split electrode 2х3,0 mm | |
| Welding power source | Lincoln Electric | |
| 3. | Operating air pressure , MPa | 0,6 … 0,8 |
| 4. | Installed capacity, kW | 7 |
| 5. | Overall dimensions, mm | 17200х4650х2330 |